
Pre-welding Preparation
1. Check and debug the equipment to ensure it is operating normally;
2. Prepare φ4.0 J402 welding rods, preferably dried at 300℃-350℃ for one hour.
Welding Process
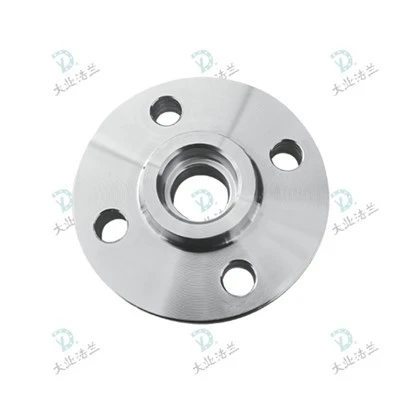
1. Assembly: Assemble the cone and large flange according to the drawings, then divide the large flange into 8 equal parts.
2. Welding: Due to the thickness of the flange and the large bevel, segmented symmetrical multi-layer welding is adopted.
Weld Quality
The weld strength must at least reach the strength of the base material. The weld surface should be smooth and free from defects such as burn-through, porosity, weld leakage, slag inclusion, undercut, and incomplete welding. The reinforcement height should be less than 2mm.
Precautions
1. When welding the root pass, always use J506 welding rods for manual surfacing and use low current welding. Strictly follow the welding process.
2. After welding each position, use a spirit level to check the deformation of the flange surface.
3. While welding, use a pneumatic hammer to tap the weld to relieve stress.