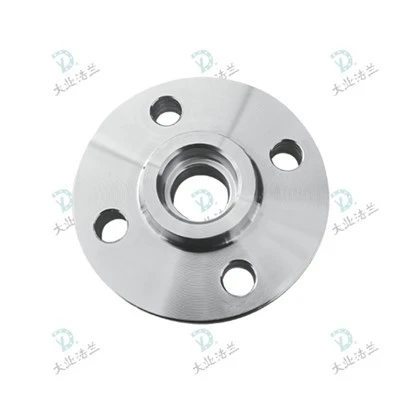

The forging process generally consists of the following steps: selecting high-quality steel billets, heating, forming, and cooling after forging. Forging methods include free forging, die forging, and mold forging. During production, different forging methods are selected based on the size of the forging and the production batch.
Free forging has low productivity and large machining allowance, but the tools are simple and versatile, so it is widely used for forging simple single-piece and small-batch forgings. Free forging equipment includes air hammers, steam-air hammers, and hydraulic presses, suitable for small, medium, and large forgings, respectively. Die forging has high productivity, simple operation, and is easily mechanized and automated. Die forgings have high dimensional accuracy, small machining allowance, and a more reasonable fiber structure distribution, which can further improve the service life of parts.
The basic steps of free forging: In free forging, the shape of the forging is gradually formed from the billet through a series of basic deformation processes. The basic steps of free forging include upsetting, drawing, punching, bending, and cutting.
1. Upsetting: Upsetting is the process of forging a blank axially to reduce its height and increase its cross-section. This process is commonly used in forging gear blanks and other disc-shaped forgings. Upsetting is divided into full upsetting and partial upsetting.
2. Drawing: Drawing is a forging process that increases the length of the blank and reduces its cross-section. It is typically used to produce shaft blanks, such as lathe spindles and connecting rods.
3. Punching: A forging process that uses a punch to punch through or through holes in the blank.
4. Bending: A forging process that bends the blank into a certain angle or shape.
5. Twisting: A forging process that rotates one part of the blank relative to another part by a certain angle.
6. Cutting: A forging process that divides the blank or removes the sprue.